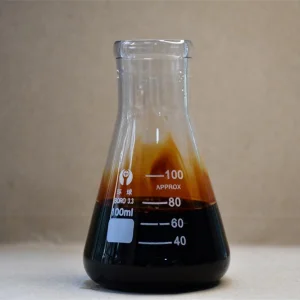
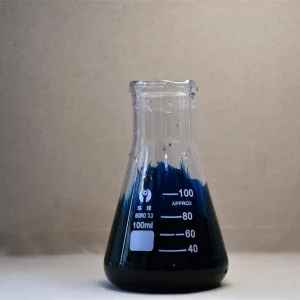
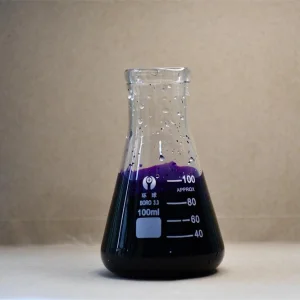
As Santana continues to emerge as a strategic hub for specialized chemical manufacturing, the demand for high-performance Liquid Dyes has surged. Unlike traditional powder dyes, liquid formulations offer superior solubility, reduced dusting, and automated dosing capabilities, critical for modern paper and textile mills.
Santana’s local industry is pivoting toward sustainability and efficiency. Our factory leverages cutting-edge Chinese chemical engineering to bring high-yield, low-waste colorants to the local market. By integrating ZDHC Level 3 and GOTS certified processes, we ensure that Santana’s paper manufacturers meet international export standards.
They provide instantaneous dispersion, eliminating the need for complex dissolution tanks and significantly improving color consistency during high-speed production runs.
 Sunrise